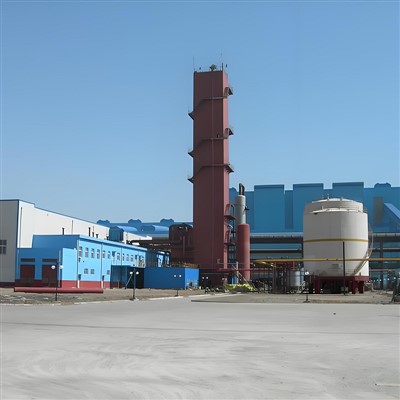
NEWTEK has successfully delivered more than 4,000 air separation units in more than 90 countries around the world, and has accumulated valuable experience from more than 550 air separation unit (ASU) operations. In the past 10 years, our total cost of ownership for plant operations has decreased by 19%, while the average power consumption of ASUs has also decreased by 15%. We offer a full range of solutions from containerized and modular ASUs to customized plants to meet the needs of more complex and challenging projects. All key components are produced in-house to ensure equipment reliability and low life cycle costs.
Air Separation Plant Support Services and Solutions
NEWTEK offers a comprehensive portfolio of services and solutions designed to solve the various problems faced by customers in air separation and hydrogen production plants. Our team always puts safety, reliability and operational efficiency first to provide customers with the best solutions.
If you need support with cold box services, our team of experts is on call at any time to provide services such as new installations, replacements, maintenance and repairs.
From plant assessments to engineering studies, maintenance technology packages, operator training and spare parts management, we provide you with comprehensive pre-sales and post-sales support to ensure smooth and worry-free production operations.
Air Separation Unit (ASU): Working Principle and Application
Air separation units (ASUs) separate air through liquefaction and distillation processes, with fractional distillation being the primary separation technology.
1. Compression
During this phase, outside atmosphere is drawn into the ASU and pressurized by a series of compressors. The purpose of pressurization is to increase the efficiency of the subsequent cooling and separation processes, with typical operating pressures ranging from 5 to 10 barg.
2. Purification
Before further processing, the compressed air needs to be purified to remove impurities (such as moisture, carbon dioxide, and trace contaminants). This process ensures that the separated gas is of high purity and prevents freezing or clogging of cryogenic equipment during subsequent operations.
3. Cooling
The purified compressed air is fed into a series of heat exchangers and refrigeration cycles to cool it to cryogenic temperatures. This process liquefies the air, as cryogenic distillation relies on differences in the boiling points of different components.
4. Separation
After liquefaction, the cold air enters a distillation tower (or multiple distillation towers) where the components are separated based on their boiling point differences:
Nitrogen has a lower boiling point (-196°C or -321°F) than oxygen (-183°C or -297°F).
If argon is present, its boiling point is even lower (-186°C or -303°F).
As the air rises in the tower, it is gradually heated and the different components evaporate at their respective boiling points. For example, oxygen-rich vapor will rise to the top of the tower, while nitrogen-rich liquid will accumulate at the bottom. If argon is present in the tower, it is usually extracted as a by-product at the midpoint of the tower.
5. Collection, storage and transportation
The separated gas is collected and sent to storage tanks, either pressurized or cryogenic. After that, the gas is distributed according to different purity requirements and supplied to various industries and different application scenarios.
In this series of operations, the efficient operation of the air separation unit is crucial, and the heat exchanger and separation tower are tightly integrated to ensure optimal working efficiency. Choose NEWTEK's air separation unit to help you meet your gas production needs.
Hot Tags: air separation plant, China air separation plant manufacturers, suppliers, air separation for web application development, air separation for artificial intelligence, air products air separation unit, air separation for data protection, nitrogen production negotiation, gas separation upgrade