

Advantages:
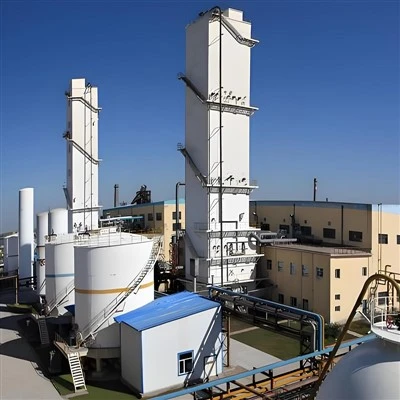
Mine Oxygen-Enriched Air Separation Unit is widely used in high oxygen-consuming industries such as copper smelting, steel, and chemicals. It offers stable high-purity oxygen output, low energy consumption, and reliable operation, meeting the continuous operation requirements of smelting furnaces. Simultaneously, the byproducts of nitrogen and liquid oxygen enhance overall economic efficiency, support environmental compliance, and achieve a dual improvement in energy saving and production efficiency.
Our services encompass:
Choosing NEWTEK gives customers more than just equipment; it provides a complete gas engineering solution:
Engineering design and process simulation
Equipment manufacturing and global sourcing
Plant layout planning and civil engineering guidance
Cold box construction and piping integration
Electrical, automation, and control systems
Operator training and long-term technical support
As a full-service provider, NEWTEK delivers complete lifecycle support for every Copper mine oxygen-enriched air separation unit-from plant layout planning and process design to automation systems, energy optimization, operator training, and after-sales service. This ensures that each unit operates smoothly from start-up, maintains long-term stability, and fully complies with environmental and safety standards.
For copper smelting plants seeking reliable capacity expansion, energy savings, and operational efficiency, NEWTEK provides a truly integrated, one-stop turnkey solution. By choosing NEWTEK, clients gain the expertise of a world-class manufacturer capable of delivering high-performance it systems tailored to their production and operational needs.

FAQ
Can NEWTEK customize the Copper mine oxygen-enriched air separation unit for different production capacities?
Yes. NEWTEK provides fully customized solutions to match your required oxygen output, purity, and production scale. Whether your copper smelting plant needs a small-scale unit or a large industrial system, we adjust the process configuration, cryogenic column size, automation level, and storage capacity to meet your operational requirements.
Can the plant layout and equipment be tailored to fit my existing copper smelting infrastructure?
Absolutely. NEWTEK's engineering team customizes the layout and integrates the Copper mine oxygen-enriched air separation unit with your existing compressors, storage tanks, pipelines, and filling stations. This ensures efficient installation, optimal space utilization, and seamless operation without disrupting current production.
Can NEWTEK adapt the unit to comply with local safety and environmental regulations?
Yes. As a global provider, NEWTEK can modify control systems, alarm logic, emergency shutdowns, and operation modes to meet local electrical standards, safety codes, and environmental requirements. Each it is tailored to operate safely, efficiently, and in full compliance with regulatory standards.
Hot Tags: copper mine oxygen-enriched air separation unit, China copper mine oxygen-enriched air separation unit manufacturers, suppliers, liquid oxygen plant performance training, mobile liquid oxygen plant, liquid oxygen trader, liquid oxygen plant output training, liquid oxygen plant logistics, liquid oxygen plant end user