

The scale of China's air separation Unit market will reach 47.87 billion yuan in 2024, accounting for more than 50% of the world's total. Companies such as Hangzhou Oxygen, NEWTEK, and Fusda are gradually increasing their market share in the international competition.
Content
3.Sichuan Air Separation Group
4.Kaifeng Air Separation (KF Group)
6.Principle of air separation unit
1.NEWTEK Group
With 3,500+ global installations, NEWTEK serves the mining, steel, chemical and other industries, with markets all over the world. It has been widely recognized for its outstanding engineering capabilities and industry contributions.
We always adhere to the concept of innovation-driven and environmentally friendly development, and are committed to carbon capture and energy-saving technologies, reducing energy consumption, achieving sustainable development, and creating a better home.

2.Hangyang Group
Founded in 1950, it is the leader in the domestic air separation equipment industry and a listed company on the Shenzhen Stock Exchange (stock code: 002430).
Its products cover the entire industry chain of "engineering general contracting-equipment manufacturing-gas operation", and are exported to more than 40 countries around the world, with a market share of 43.21% in 2020.
Representative technology: Extra-large air separation equipment, widely used in steel, chemical and other fields, and actively expanding overseas markets.
3.Sichuan Air Separation Group
Founded in 1966, with cryogenic technology as its core, its business covers air separation equipment, natural gas liquefaction and other fields.
The engineering sector includes complete sets of equipment and technical services for air separation and natural gas liquefaction systems, and its technical strength ranks among the top in China.
4.Kaifeng Air Separation (KF Group)
Founded in 1958, it is affiliated to Henan Energy and Chemical Industry Group and focuses on large and medium-sized air separation equipment and gas liquefaction supporting equipment.
Products include high-pressure coil heat exchangers, natural gas separation and liquefaction units, etc., and it is a backbone enterprise in the domestic air separation equipment manufacturing industry.
5.Fortune
Founded in 1984, it has been deeply engaged in the field of cryogenic technology and provides system solutions such as air separation and natural gas liquefaction.
It has delivered more than 700 air separation units in total, with outstanding performance in overseas markets. In 2023, overseas sales of low-temperature petrochemical equipment accounted for 53%.

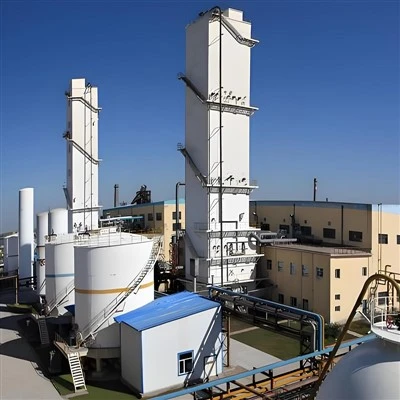
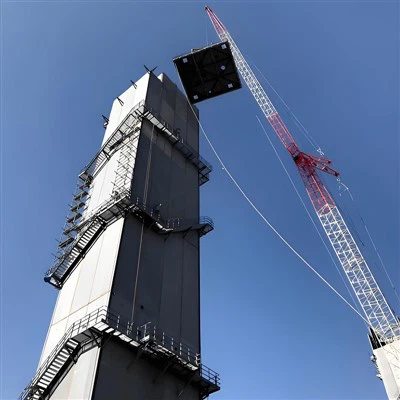

6.Principle of air separation unit
1. Cryogenic method (low-temperature distillation method)
Core principle: Utilize the difference of boiling points of components such as oxygen and nitrogen (oxygen boiling point -183℃, nitrogen boiling point -196℃), and achieve separation through compression, liquefaction, distillation and other steps.
Air compression and purification:
The air is pressurized to 5-10 bar (gauge pressure) by the compressor, and impurities such as water, carbon dioxide, hydrocarbons, etc. are removed by molecular sieve adsorbent.
Cooling and liquefaction:
The compressed air is pre-cooled to near liquefaction temperature by the reflux cold gas through the main heat exchanger, and then further cooled and liquefied by the expander or throttle valve.
Distillation separation:
Liquid air enters the two-stage distillation tower (high pressure tower and low pressure tower):
High pressure tower: oxygen-rich liquid air accumulates at the bottom of the tower, and nitrogen is condensed into liquid nitrogen at the top of the tower.
Low-pressure tower: Liquid nitrogen is used as reflux liquid, and oxygen-rich liquid air is further evaporated and purified to finally obtain high-purity oxygen (more than 99.6%) and nitrogen (<1 ppm impurities).
Technical features:
High energy consumption, but high product purity (oxygen purity can reach 99.8%).
Suitable for large-scale industrial production (such as metallurgy, chemical industry).

2. Adsorption method (molecular sieve/pressure swing adsorption)
Core principle: Utilize the selective adsorption difference of molecular sieves for nitrogen and oxygen. For example:
Carbon molecular sieves preferentially adsorb oxygen and discharge nitrogen-rich gas (purity 90-99.9%).
Zeolite molecular sieves preferentially adsorb nitrogen and output oxygen-rich air (oxygen content 70-93%).
Technical features:
Simple process and low energy consumption, but the product purity is lower than that of cryogenic method.
Suitable for small and medium-scale nitrogen production or oxygen-enriched needs (such as medical treatment and combustion optimization).
3. Membrane separation method
Core principle: Utilize the permeation selectivity of organic polymer membranes. The oxygen permeation rate is 4-5 times faster than that of nitrogen. It is separated by pressure difference and outputs oxygen-rich gas (28-35% O₂).
Technical features:
The equipment is compact and has no moving parts, but the purity is low, which is suitable for low-purity scenarios (such as aquaculture).
IV. Technical optimization and development
Energy saving improvement:
The structured packing tower is used to reduce resistance and reduce air compressor energy consumption.
The expander recovers cold and improves energy efficiency.
Intelligent control:
The DCS system realizes full process automatic monitoring, and remote operation and maintenance improves efficiency .
Impurity treatment:
The spiral degassing device and microbubble separator remove tiny bubbles and particulate impurities to protect the equipment.


